Platinum
Takes the beam in and holds the heat where it lands. The pool stays compact and the metal a short distance away stays cool.
M3 · one QCW source, seven metals
One dial, three metals, trimmed on the first shot.
One laser welder — gold, silver, platinum, titanium, copper, aluminium and steel — from a single QCW source running at 120 W (1,200 W peak), with the welding spot adjusted by motor from 0.1 to 2.0 mm.
Swipe the scale →
Takes the beam in and holds the heat where it lands. The pool stays compact and the metal a short distance away stays cool.
Moves along the scale with the karat on the hallmark. 22K behaves far closer to silver than 9K does.
Throws more of the beam back and drains what does get in faster than anything else on the bench.
The scale
Every difference between these metals comes down to two things: how much of a 1064 nm beam the metal takes in rather than throwing back, and how fast the heat leaves the joint once it is in.
Melts high, so the shot has to carry real energy, and what it carries stays put. The boundary between melted and unmelted metal is tight.
Where it sits depends on what is alloyed with it: the higher the gold content, the more the metal reflects and the faster it moves heat.
More of the beam comes back off the surface, and what does go in leaves the joint faster than in any other metal here.
The shot that makes a bright melt point on platinum can leave silver looking barely touched, and the next step up can flood it. That is why this page is organised by alloy, not by job.
Alloy families
The hallmark tells you how much precious metal is in a piece. It does not tell you what else is in there, and that is what behaves at the weld.
Each family sits somewhere on this scale
| What the customer calls it | What is in it besides the precious metal | What that does at the weld |
|---|---|---|
| Fine silver, 999 | Almost nothing | Brightest silver pool, no copper oxide, the most heat-hungry metal on this list |
| Sterling, 925 | Copper | Fire stain around the weld zone, casting porosity that opens when re-melted |
| Germanium-bearing sterling | Copper plus germanium | Behaves close to sterling, holds colour better around the heated area |
| 22K and 21K yellow | Small amounts of silver and copper | Soft, fluid pool, close to fine silver in how it takes the beam |
| 18K yellow, 750 | Silver and copper | The most predictable gold family, and the widest working window |
| 14K, 10K and 9K yellow | More copper, silver, zinc | Zinc-bearing alloys spit, and oxide colour spreads further from the point |
| Rose and red gold | Copper-dominant | Colour shifts around the weld, more prone to cracking when worked hot |
| Nickel white gold | Nickel, sometimes zinc | Hard, work-hardens, the white gold most likely to crack at a stressed joint |
| Palladium white gold | Palladium | Softer, greyer, forgiving pool, close to platinum in temperament |
| Platinum 950 with ruthenium | Ruthenium | The common fabrication alloy, welds and finishes to itself without oxide |
| Platinum 950 with iridium | Iridium | Softer pool, with more movement under the same shot |
| Platinum 950 with cobalt | Cobalt | Cast alloy, finer grain, slightly magnetic, not the ruthenium alloy's twin |
| Gold-filled, rolled gold, plated | A base metal core under a precious layer | The core is what you weld, and it is usually what the customer did not mention |
Where a piece could be either of two families, set for the harder of the two and trim down after the trial shot rather than up.
Where the customer cannot tell you which it is, normal on inherited pieces, that is a question for a hidden trial spot on the piece, not for the counter.
 Pending photo · mark and no more
Silver
Silver is the metal people ask about before they buy a machine, and they are right to ask.
It sits at the far end of both orders, so a silver joint wants a spot open enough to build a pool before the surrounding metal drains it.
Closing the spot right down and firing repeatedly, the instinct carried over from prong work in gold, gives a row of small craters that never join.
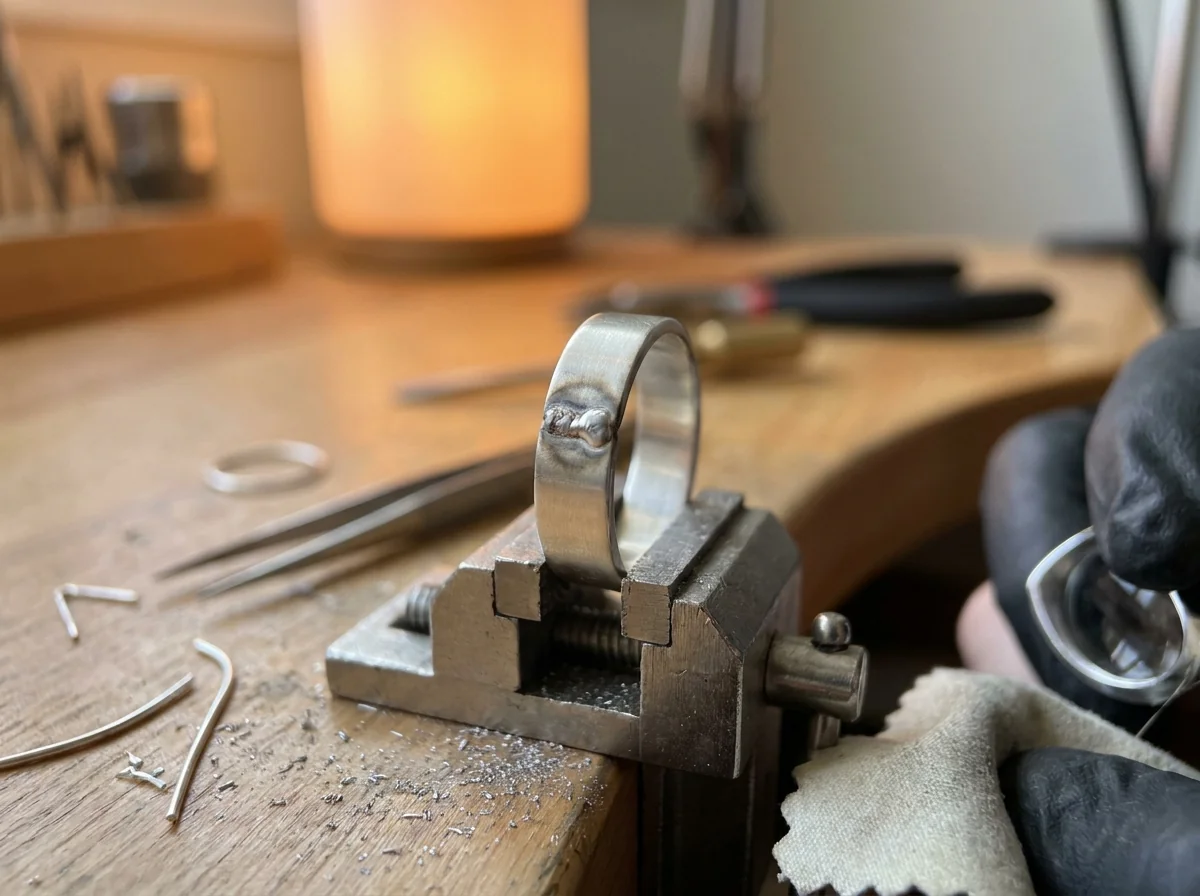
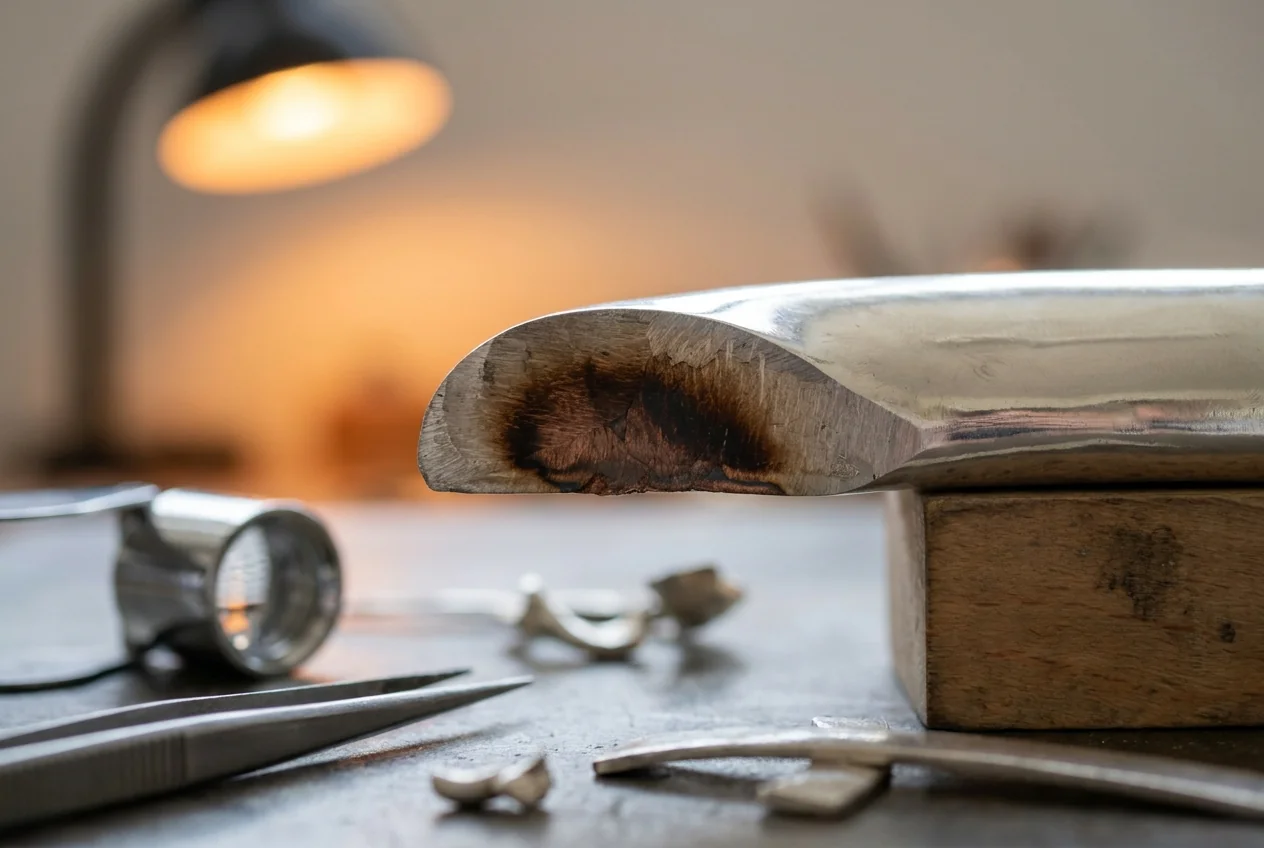
Copper oxidises below the surface wherever the metal has been heated, and on silver it shows as a grey shadow the polishing wheel will not lift.
Cast sterling carries gas, and re-melting lets it out through the pool. The answer is a re-melt with less energy, not more metal stacked on top.
No copper, so no fire stain and no grey. It is also the hungriest metal here, with nothing in it to slow the heat down.
A laser weld puts heat into a far smaller area than a torch does, so the stain is a ring around the joint rather than a whole shank.
Silver work at the repair counterKarat gold
Karat gold covers the widest behaviour range of anything on this page, and the single number on the hallmark is what tells you where in that range you are.
Swipe the scale →
More of the beam comes back and heat moves faster, so the pool is fluid once it goes. Soft after welding, so a high karat shank wants more support from the piece itself while you work.
A trial shot reading slightly off still gives a usable weld, colour match at the joint is good, and one setting carries across a run of similar pieces.
Zinc boils below the temperature the gold melts at, so it leaves the pool as vapour and the melt point spits. Oxide colour also spreads further from the weld.
Copper-dominant, so colour shifts around the heated area, and these are the golds most likely to crack at a joint already stressed by a previous sizing.
If you are learning the machine, learn it on 18K.
Spitting on a low karat piece is the alloy talking, and the correction is less energy over more shots rather than pushing through it.
Karat chain work in front of a customerWhite gold
White gold is two different metals sold under one name, and the difference shows up at the weld before it shows up anywhere else.
Nickel white
The property jewellers value in a head is the one that causes trouble at a repair. A shank sized twice carries a joint harder and more stressed than the metal beside it.
Palladium white
The pool is far more forgiving, and it sits close to platinum in temperament. It is increasingly what newer pieces are made of, without the customer knowing which one they own.
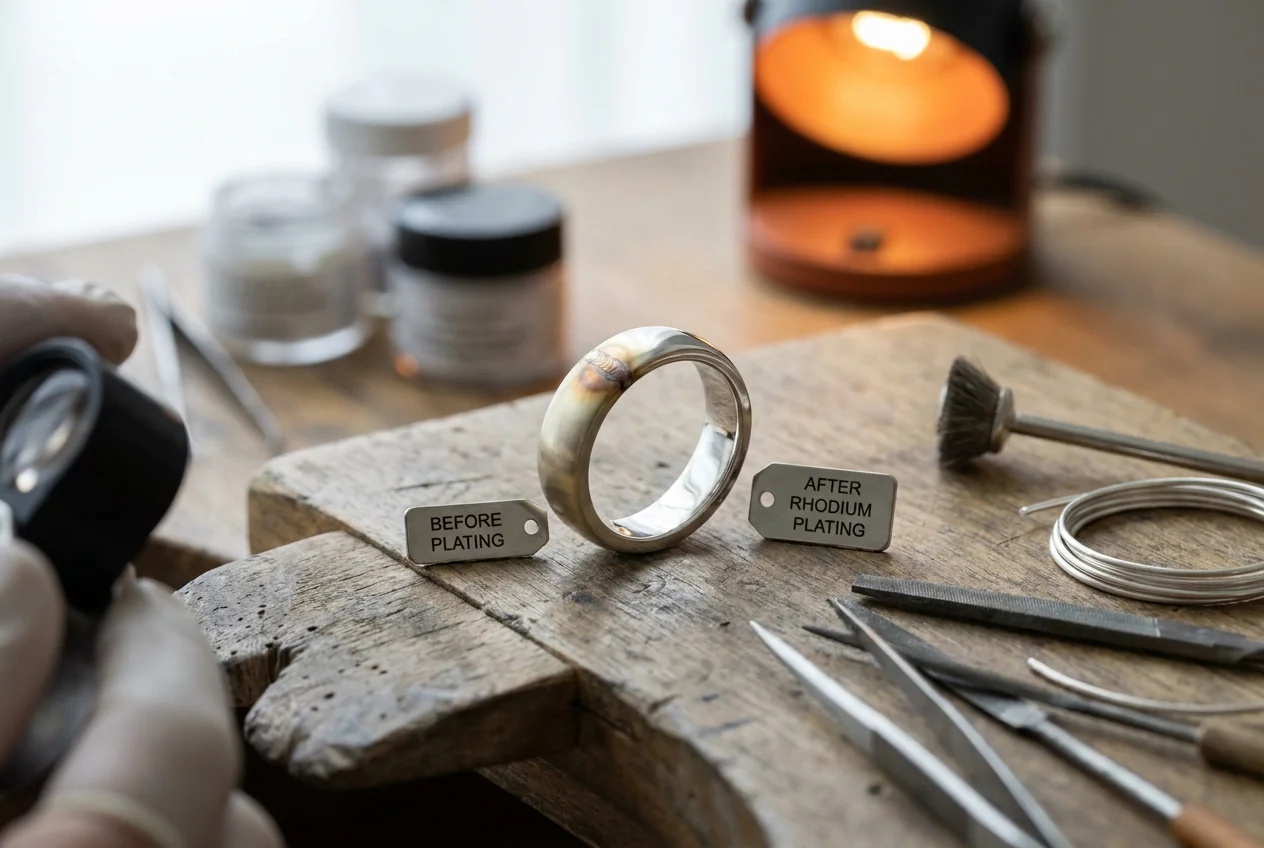
Both are almost always rhodium plated. The weld strips plating around the joint, and a white gold piece that leaves a laser bench unplated shows a warmer patch exactly where the repair was.
A piece that comes in rhodium plated goes back out rhodium plated, planned for when the job is quoted rather than discovered at the polishing motor.
Platinum 950
Platinum is the metal laser welding suits best, worth saying plainly when most of this page is about difficulty.
It takes the beam in and holds the heat where it lands, so the melted zone stays tight and the metal a short distance away stays cool. It does not oxidise at welding temperature in air the way silver and the copper-bearing golds do.
Welded with metal of the same alloy, the joint finishes to the same colour and polish as the parent metal and disappears rather than being disguised. Torch and solder put a different alloy of a different colour into that joint.
Same alloy, same colour, same polish, and no oxide to lift afterwards.
There is no platinum position on the dial, and we are not going to pretend there is.
The material dial
A preset is a starting point for a class of metal, and it is worth being precise about what that means.
The metal family in front of it: how much of the beam that family takes in, how fast it drains heat away, and where in the machine's range a first shot ought to sit.
The individual piece. None of the following is on the hallmark, none of it is in a preset, and all of it changes the shot.
One press loads the starting point for that family and puts you within reach of the joint.
Put it where it will be finished away or never seen, and read it under the microscope.
Adjust against what the first shot shows you, then work the joint with the answer in hand.
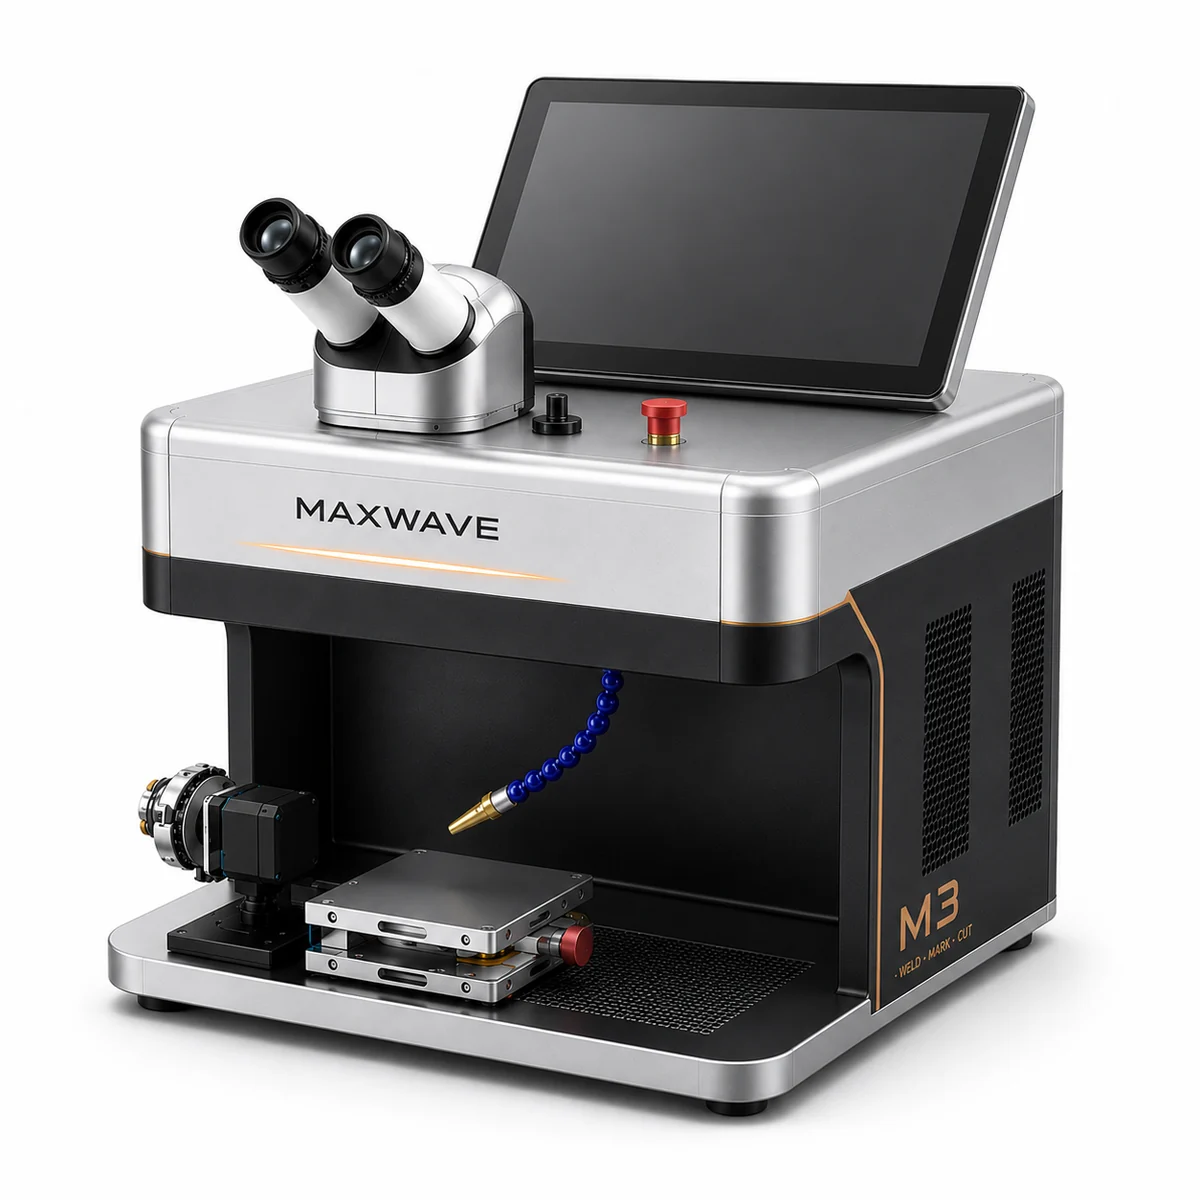
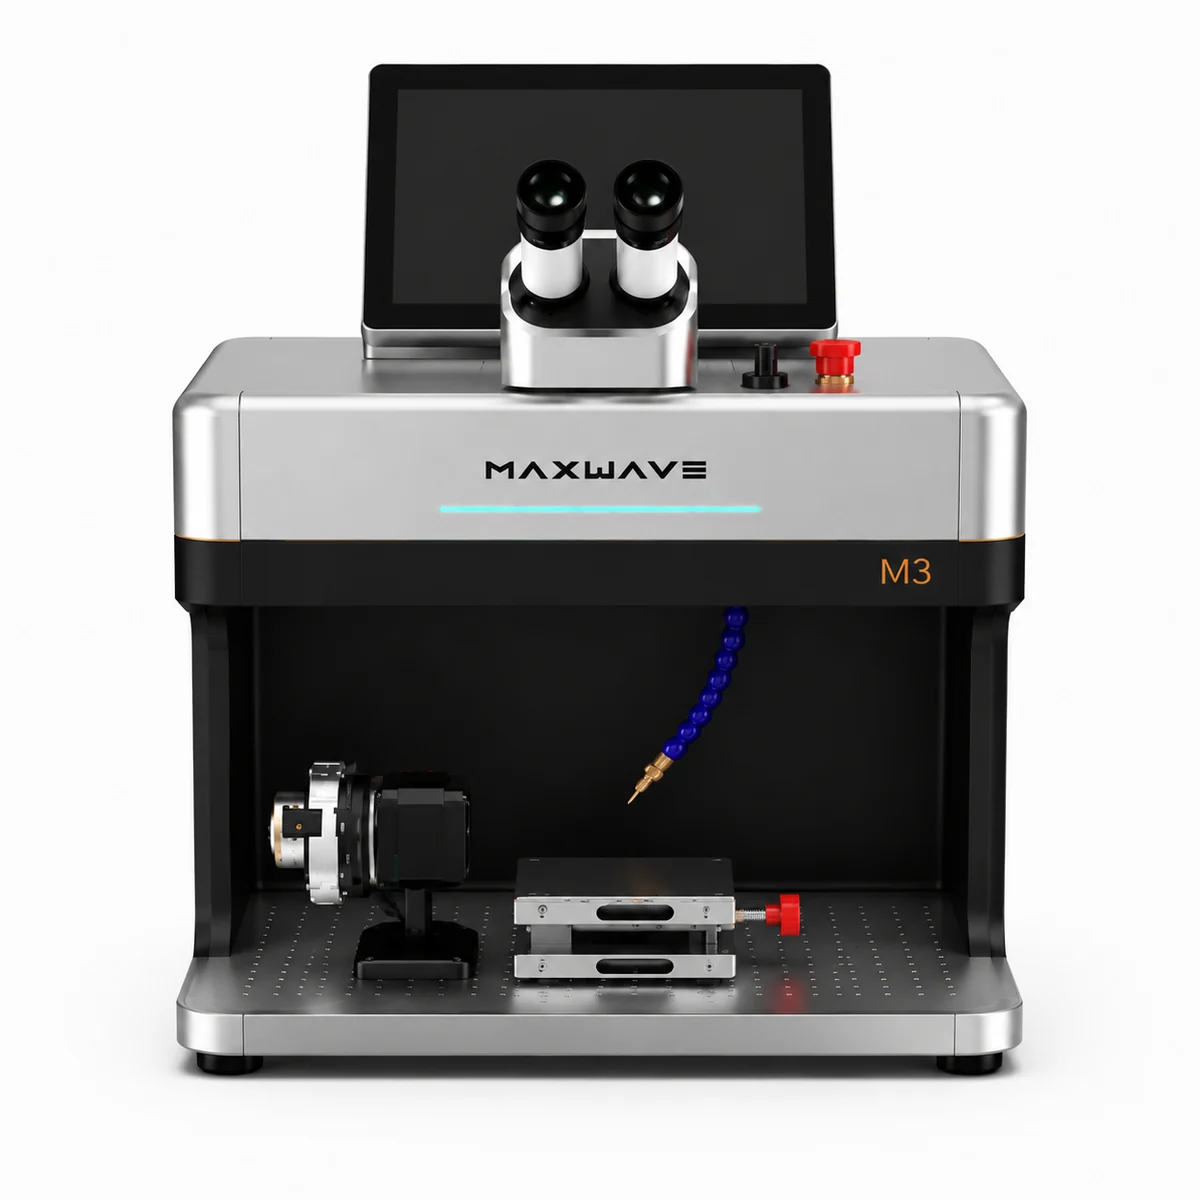
10 inch Android screen · where the dial lives
Metals without a position of their own, platinum among them, start from the nearest position and reach the same place by the same route: one trial shot, read, trimmed.
Holding
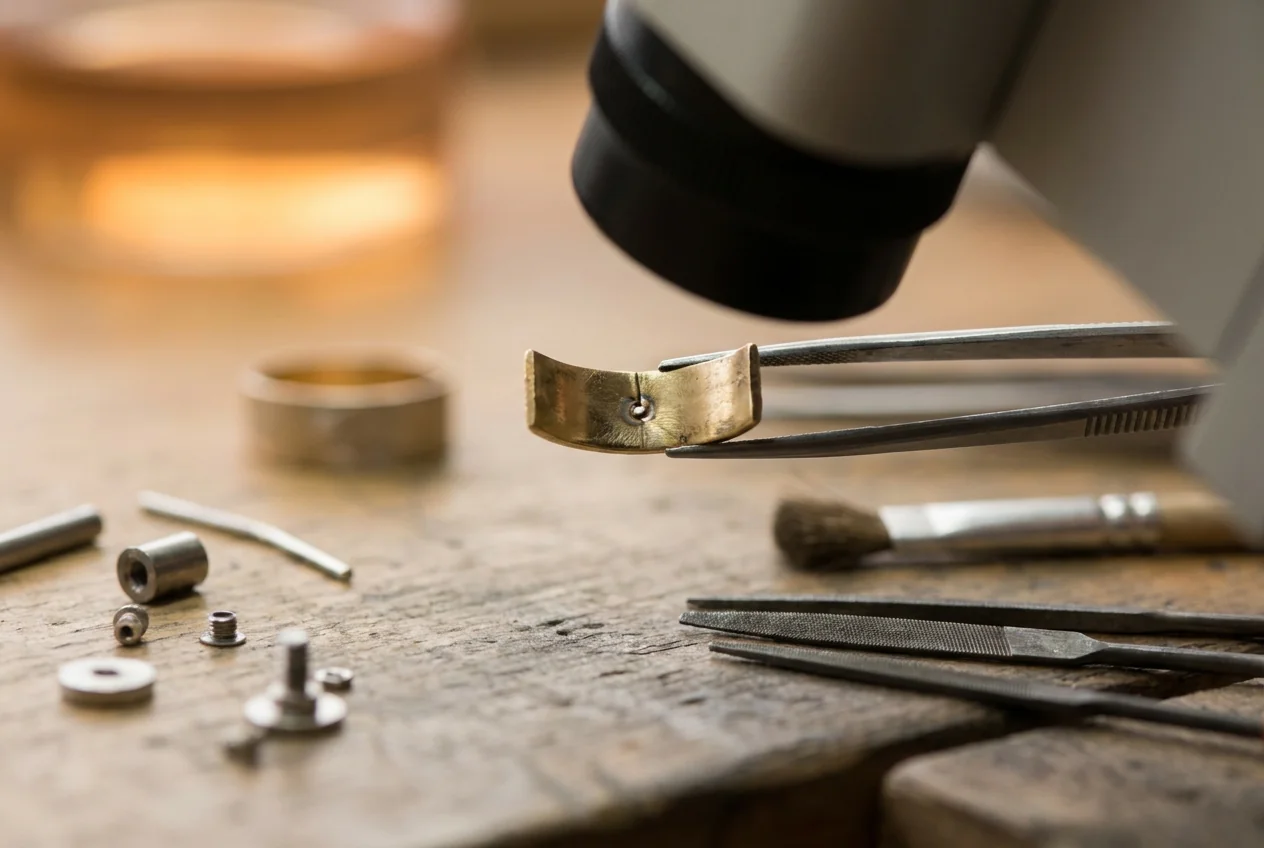
Where the heat goes after it enters the piece is a holding question, and it has a different answer for each of these metals.
The piece is its own sink
Heat leaves the joint so readily that a steel tweezer nearby does less than people expect, and a heavy holder can pull enough heat out that the pool will not form at all.
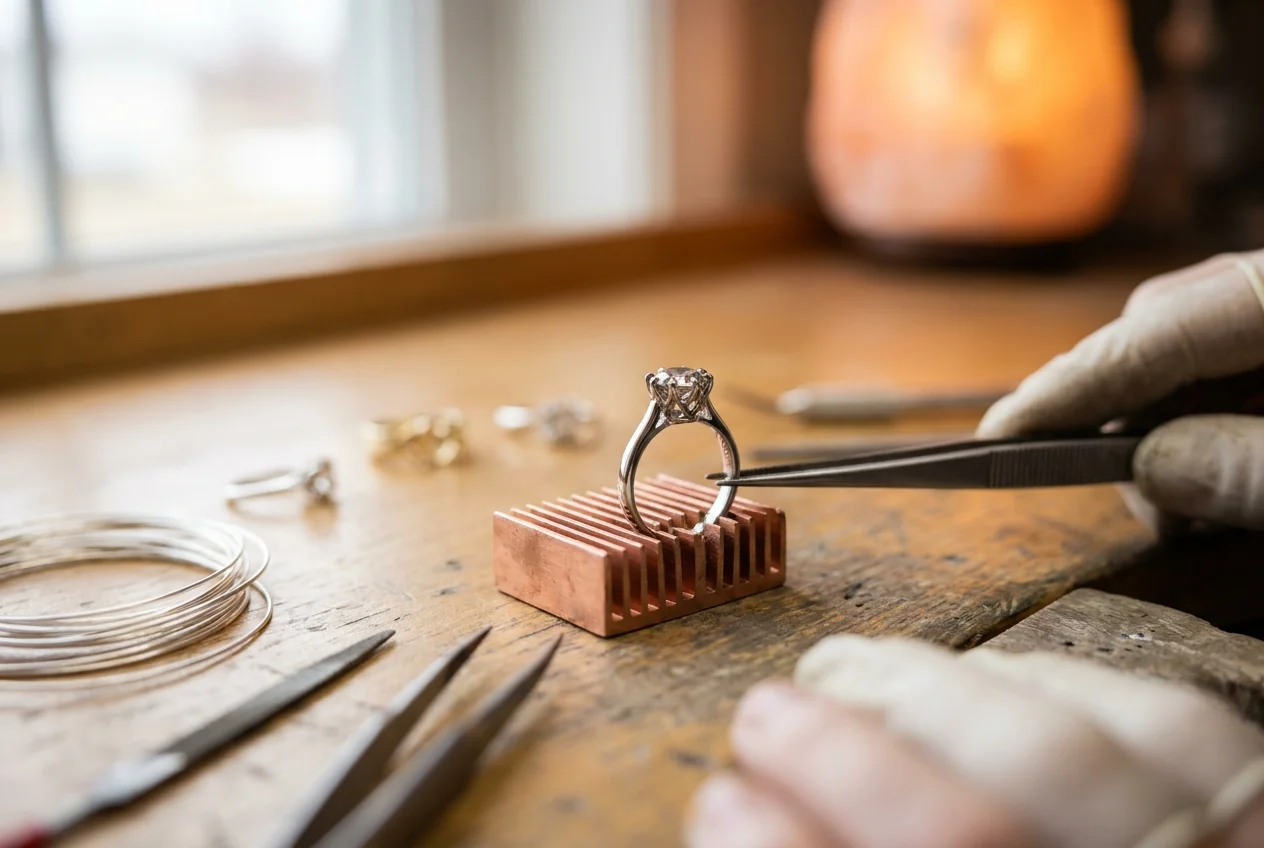
A sink works, and works locally
Heat stays where it lands, so a sink between the joint and something that must stay cool does its job. The same property lets you work close to a setting.
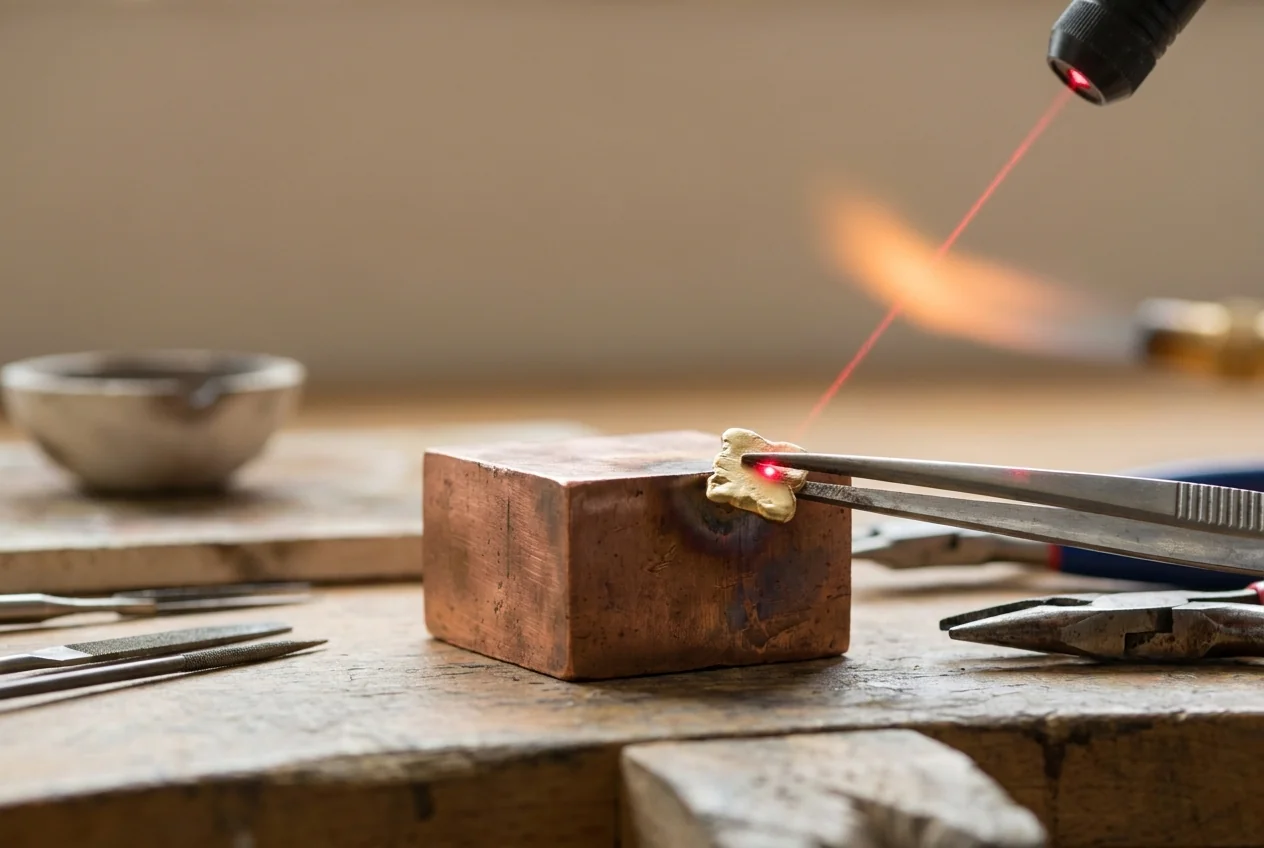
Shifts with the karat
On low karat pieces with a lot of base metal, a sink in the heat path works well. On 22K it behaves more like silver and wants the lighter hold.
After the weld
What leaves a laser welder — gold, silver or platinum — still needs finishing, and that belongs in the quote rather than being discovered later.
Rose gold shifts colour around the heated area on its own account, and wants the finishing to run slightly wider than the weld to blend it.
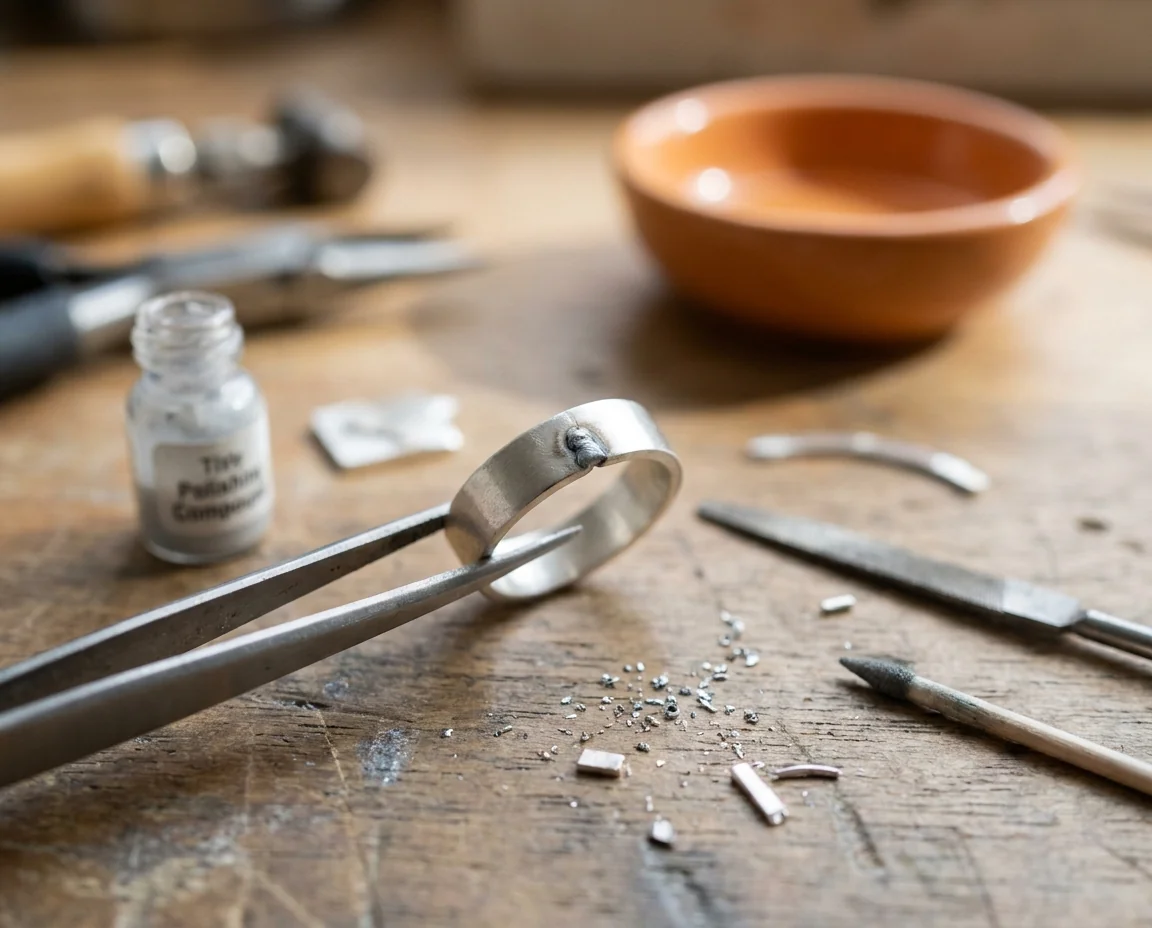
The joint, at the setting the trial shot gave you.
At magnification, before anything is dressed away.
The area, not the piece, and only as wide as the metal asks.
Again, because finishing can open what welding closed.
Finding a problem on the first joint of four is a repair; on the last it is a rebuild.
Two metals, one joint
A silver piece with a gold accent, a gold chain with a steel spring ring, a platinum head on a gold shank. Bias the aim toward the higher melting, slower conducting side and let the pool come to the other one.
Favour the gold side. The silver drains heat away faster, so splitting the shot down the middle melts one side into a puddle while the other stays solid.
Favour the steel finding. Spring rings, clasps and pins hold heat where it lands, so the pool builds there and reaches the softer side.
Favour the platinum. It melts higher and holds its heat, so it takes the energy the gold side cannot be given without moving.
A base metal core under a thin precious layer, so welding them is welding the core, with the layer around the joint gone. Tell the customer before the machine is switched on.
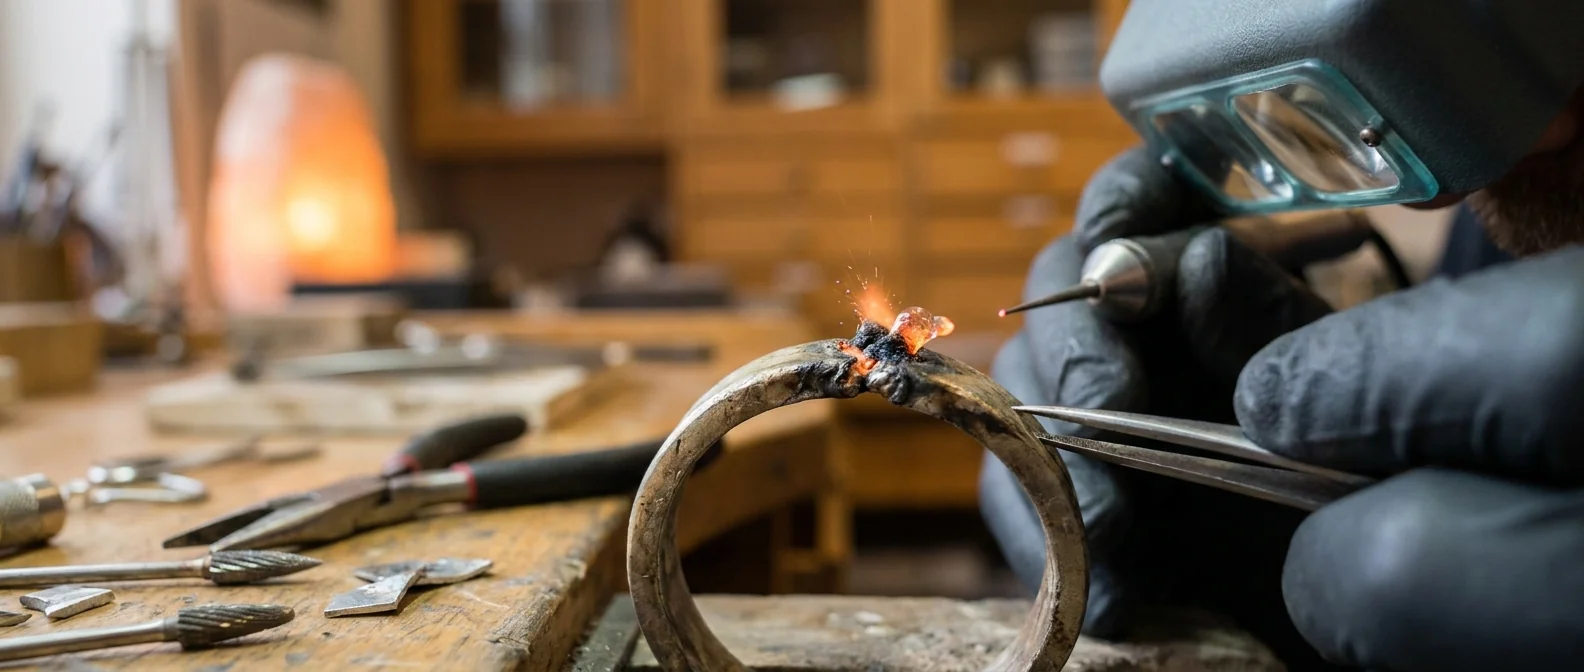
A joint repaired before holds a third alloy, usually lower melting and often carrying zinc. That is why those joints spit when they are welded over.
Same source
What we do not publish
That table does not exist on our side yet, and we would rather say so than invent one.
A number printed against a metal name is a promise about a piece nobody has looked at. The limit moves with the mass of the piece, how that mass sits, what is holding it, and which alloy family it is.
A heavy fine silver cuff and a light 18K shank of the same wall thickness are not the same job, and that cuff cast with porosity in it is different again.
So send the item, or an offcut of the same alloy at the same section. It goes on an M3 on our bench, and comes back with the weld in it and the settings beside it.
The answer is about your metal, not a sample we chose.
Start with your own alloyWhat to send
Six things make a test piece worth running, and five of them are information rather than metal.
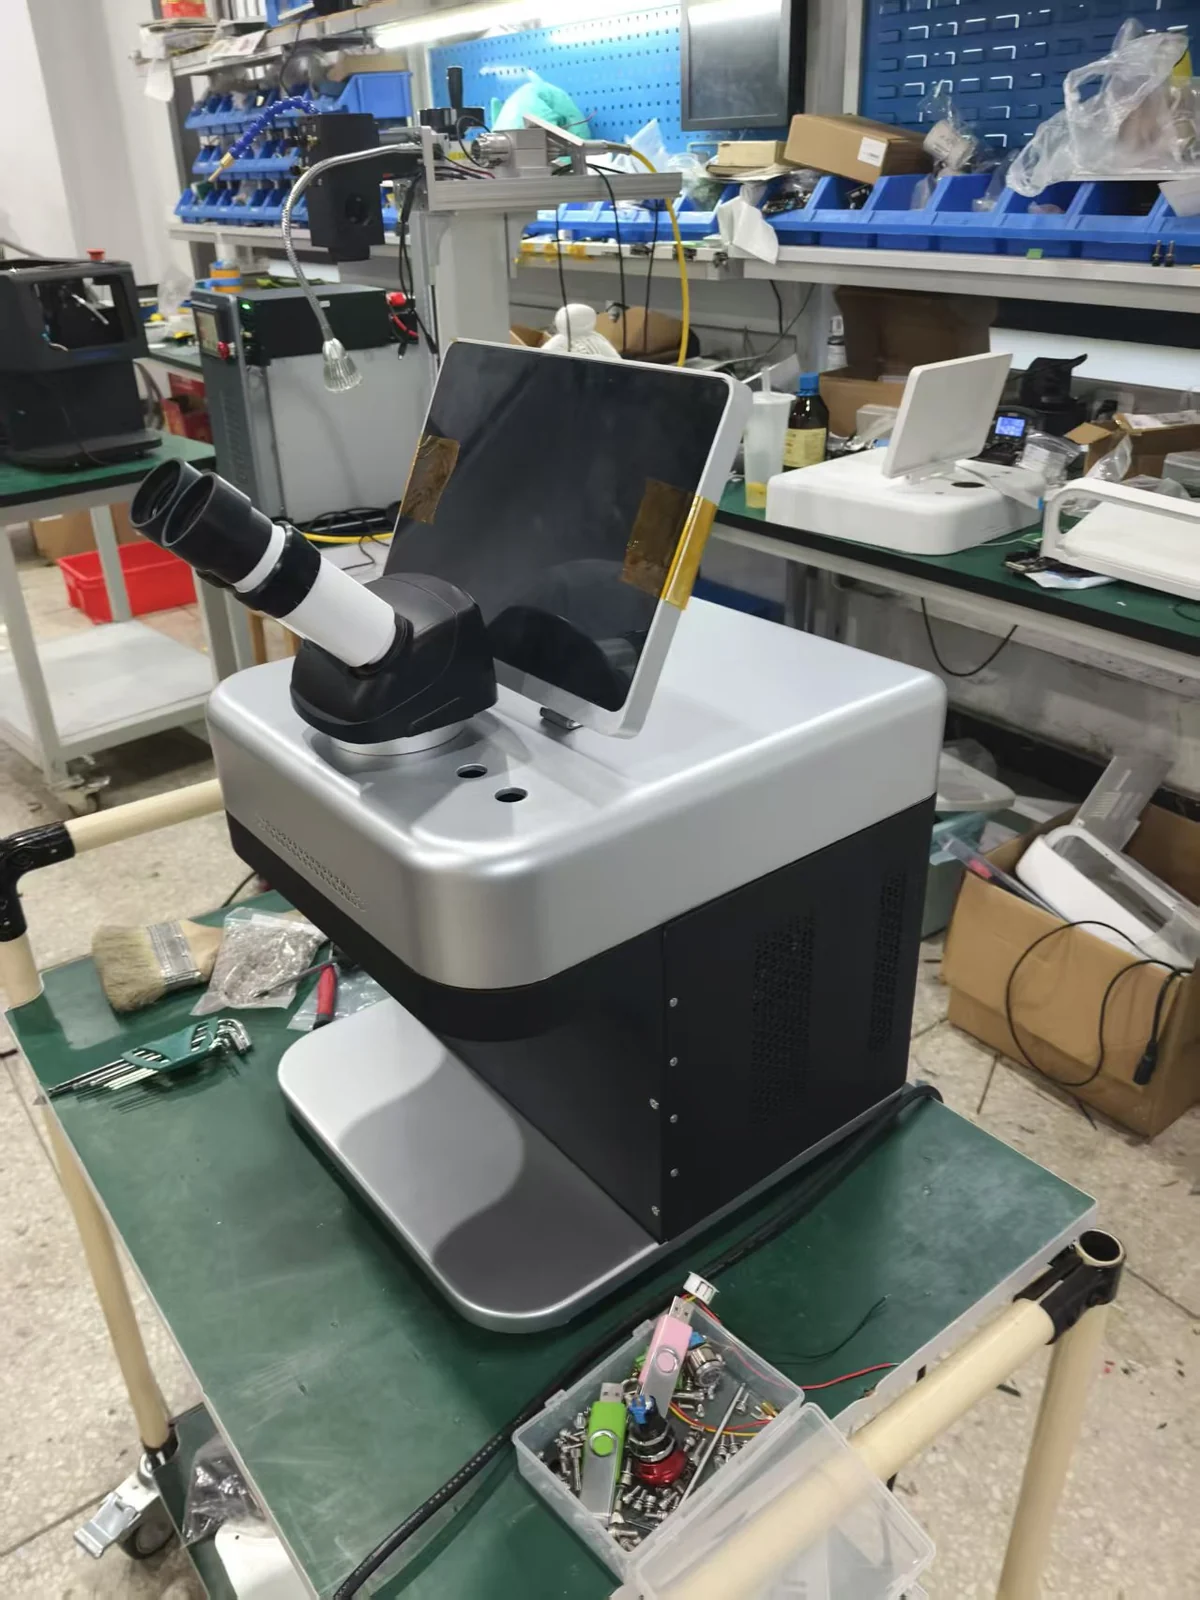
Your piece goes on an M3 on this bench, not on a coupon we chose.
Your metal with the weld in it, so you can put it under your own loupe and your own wheel, with the settings that made it and a note on anything the alloy did.
Pending photo · piece and settingsSend a welding test
Send a piece in the alloy you actually work in, or an offcut of the same stock at the same section, and tell us the joint you want made. It comes back welded, with the settings written down.